Hot Air Heaters for Carton and Paper Cup Sealing
TUTCO SureHeat has built electric air heaters for OEM production equipment for more than 25 years, from a few kilowatts to multi-megawatt systems, and at outlet temperatures above 1050 C (1922 F). One of the oldest and highest-volume uses of that technology is heat sealing polyethylene-coated paperboard. Every gable-top milk carton, aseptic carton, paper cup, bowl and lid gets its seal from a stream of hot air that melts the coating a fraction of a second before a jaw or a mandrel presses the joint closed. The heater that makes that air is a wear part in a machine running at thousands of units per hour, and it is also the part that decides whether the seal holds. If you build carton filling machines or cup forming machines, this page covers what the sealing heater must do and which SureHeat families fit. If you maintain those machines, it covers what to specify when you replace a hot-air element.
Why Paperboard Packaging Depends on Hot Air
Liquid food packaging is moving back toward paper. Dairy, juice, liquid egg, plant milk, broth and foodservice beverages are packed in gable-top and aseptic cartons and in paper cups because fiber-based packaging carries a lower carbon footprint than rigid plastic and is easier to position as recyclable. The fiber on its own cannot hold liquid, so the board is coated with polyethylene. That coating is also the adhesive. There is no glue in a gable-top carton seal and none in a paper cup seam. The PE is melted and the two surfaces are pressed together. That makes the heater a process-critical component rather than a utility. A gable-top filler runs 1,500 to 6,000 cartons per hour. A high-speed cup machine runs well over 100 cups per minute. Each unit gets a fraction of a second of hot air. If the air is cold the seal leaks, and a leaking milk carton is a product recall. If the air is too hot the coating degrades, the board scorches, or the molten PE smears onto tooling. The installed base is large and global. The companies building this equipment range from the long-established carton system suppliers in Europe, Japan and North America to a very large group of cup and bowl machine builders in China, India, Korea, Taiwan and Turkey. Many of them publish the sealing method openly: hot air for the bottom, hot air for the top, hot air for the seam, often two independent hot-air systems on one machine. Each of those stations contains an electric air heater, and each of those heaters is a consumable.
Where the heater sits: hot air activation of PE-coated paperboard
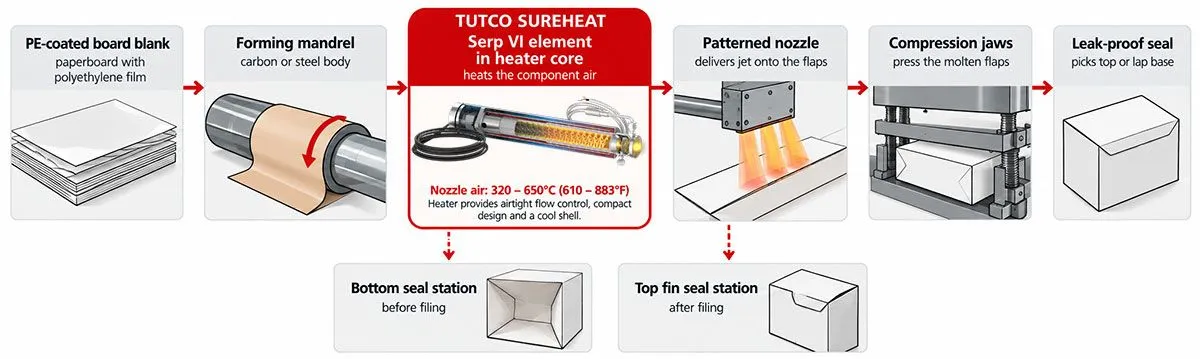
The same element type serves both stations on a gable-top line
SAFETY DETAIL: When the line stops, the ovens retract and an air knife protects the cartons, so element response time and repeatable outlet temperature matter as much as peak heat.
The element heats the air that melts the polyethylene coating just before the sealing jaws close.
What Actually Happens at the Seal
The process is a controlled, very short thermal event. A nozzle or an oven directs hot air at the flap, seam or bottom disc. The outer surface of the PE coating goes above its melting point, typically in the region of 110 to 130 C for low-density polyethylene, in a few hundred milliseconds. Then a jaw, a mandrel or a knurling tool applies pressure and the molten layers fuse.
The important point for heater selection is that the air is much hotter than the coating ever gets. Machine builders in this sector typically run 300 to 450 C (570 to 840 F) at the heater outlet for gable-top flap activation, and typically 300 to 500 C (570 to 930 F) for cup sidewall and bottom sealing. The board surface never approaches those numbers because contact time is well under a second and the paper fiber underneath acts as a heat sink. The hot air is a delivery mechanism for a measured amount of energy, not a soak temperature.
That is also why the pattern matters. Gable-top machines blow hot air in a selective pattern so that only the sealing area is heated. Heating the whole flap would soften coating where it is not wanted and waste energy. When the machine stops, the ovens retract and an air knife keeps residual heat off the cartons. The heater, the nozzle geometry and the machine motion are one system.
- PE coating is both the barrier and the adhesive, so the heater is in the seal-integrity path
- Dwell is a fraction of a second, so air temperature is far above coating melt temperature
- Heating is selective by nozzle pattern, not a bulk oven soak
- Stopping the line must remove the heat from the board, which means a retracting oven, an air knife, or both
- Air temperature, air flow and line speed must be controlled together, not independently
The Engineering Problem Specific to Hot-Air Sealing
This is a hard duty for an air heater, and the failure modes are consistent across the sector. Duty cycling is the first. A form-fill-seal machine does not run continuously. It stops for a carton jam, a reel splice, a fill fault or a shift change. Each stop is a thermal cycle on the element, and the station has to be back inside the seal window within seconds of restart or the first cartons out are scrap. An element with high thermal mass cannot do that. Open-coil construction with a fast ramp is what makes the restart acceptable.
Thermal lag against line speed is the second. The heater is controlled on outlet air temperature, but what matters is the energy delivered to the board. When the machine accelerates, the dwell at each nozzle shortens. If the control loop only watches air temperature, the seal gets less energy at speed than it did during the slow start. Closed-loop control at the heater outlet, with the setpoint tied to machine speed, is the practical fix.
Contamination is the third, and it is specific to paper. Board dust and paper fiber are everywhere in a cup or carton machine. Drawn into a heater inlet, fiber carbonizes on the coil. Deposited on a nozzle, it narrows the orifice and changes the flow. PE vapor from the seal itself condenses on cooler surfaces downstream and builds a varnish. Filtered inlet air and a nozzle cleaning interval are part of the heater specification, not an afterthought.
Flow loss is the fourth, and it is the most common cause of a burned-out element. The coil is cooled by the air passing over it. A blocked filter, a kinked hose or a partly plugged nozzle starves the element while the controller continues to call for heat. Serpentine VI, for example, requires a minimum of 60 SCFH for accurate control. Below the minimum flow the coil temperature runs away from the measured outlet temperature. Minimum flow must be guaranteed mechanically or interlocked, not assumed.
Food contact is the fifth. The air touches the inside surface of a drinking cup or a milk carton. Nothing may be added to it. Electric resistance heating of a filtered air stream adds only heat, which is the fundamental reason this process is electric and not flame-based.
- Stop-start cycling: element must tolerate frequent thermal cycles and recover the setpoint in seconds
- Thermal lag: dwell shortens as the line accelerates, so energy per seal falls unless the setpoint tracks speed
- Contamination: board dust and paper fiber on the coil, PE vapor varnish on nozzles and ducts
- Flow starvation: below minimum flow the coil overheats while the outlet thermocouple reads normal
- Nozzle-adjacent element life: the hottest, dirtiest position in the machine, so plan it as a replaceable part
- Pressure drop: a long duct or an undersized nozzle robs flow and shifts the whole operating point
- Food contact: no combustion byproducts permitted in air that touches the package interior
- Multiple stations per machine: a cup machine commonly has two or more hot-air heaters, each needing its own loop
TUTCO SureHeat Heaters for Carton and Paper Cup Sealing
SureHeat Serp VI Triple-Pass Heater
The direct replacement element for a compact hot-air seal station: cup bottom nozzles, cup sidewall seam preheat, and gable-top top and bottom flap heaters. This is the part most maintenance engineers in this sector are actually shopping for.
- Rated to 1500 F (815 C) outlet air, well above the typical 300 to 500 C sealing setpoint, so the element runs with margin rather than at its ceiling
- Power options of 5.0 kW, 6.0 kW and 8.0 kW, which covers a single-nozzle seal station
- 240 V single-phase configuration listed, matching the control voltage available at most seal stations
- Maximum inlet pressure 25 psi, suited to blower-fed and shop-air-fed nozzles
- Minimum flow of 60 SCFH required for accurate control, which is the figure to design the air circuit against
- 304 stainless steel housing
- Triple-pass open-coil Serpentine element in a compact modular package for space-constrained stations
- Specified with digital temperature controllers and Type K thermocouples
SureHeat Jet Process Air Heater
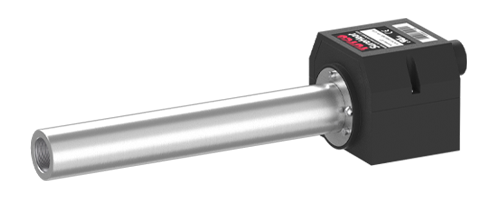
The compact designed-in air heater for a single top or bottom seal nozzle on a new machine, and the usual substitution for a small imported hot-air blower on an existing one. Its size is what makes it fit inside a crowded forming turret or a retracting oven.
- Exhaust temperatures as high as 1400 F, so the sealing setpoint sits comfortably inside the range
- Offered in 3 kW and 8 kW, which maps well to one nozzle at cup-machine flows
- Single-phase operation, so no three-phase feed has to be run to the station
- Single heating element in the 3 kW build, giving low thermal mass and a fast ramp from cold
- Dual Type K thermocouples and over-temperature protection
- Compact package for mounting close to the nozzle, which shortens the hot duct and reduces thermal lag
SureHeat Max Process Air Heater
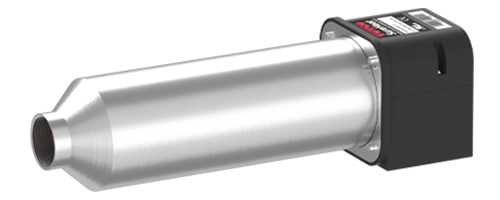
The high-output heater for a manifold that feeds several nozzles at once: a multi-lane gable-top bottom or top oven, or a high-speed container machine where one heater serves the whole seal pattern. Use it where a single-element heater runs out of power before it runs out of temperature.
- Exhaust temperatures as high as 1400 F
- 6 kW to 36 kW, with up to six heating elements in the 36 kW build
- Available in single-phase and three-phase configurations for the larger ratings
- Significantly more power per unit size than a single-element heater, which matters in a fixed station envelope
- Dual Type K thermocouples and over-temperature protection
- Suited to selective-pattern hot-air ovens where total flow, not peak temperature, sets the heater size
Specifying the Heater for a Seal Station
Six numbers determine the heater. The station envelope, because the heater has to fit inside a forming turret or a retracting oven. The mounting and nozzle arrangement, because that sets the duct length and the pressure drop. The available voltage, because a 240 V single-phase station and a three-phase station lead to different families. The airflow, because it sets the required power far more than the temperature does. The setpoint, which in this sector is typically 300 to 500 C. And the cycle rate, which sets how fast the heater has to recover. Power follows from flow and temperature rise, not from the board. A single cup-machine bottom nozzle at modest flow is a single-element job. A multi-lane gable-top oven manifold feeding several nozzles from one heater is not. That is where a multi-element heater earns its place, because it delivers more power in the same station envelope.
Temperature headroom is worth paying for. Running an element rated to 1500 F at a 450 C setpoint means the coil is nowhere near its limit, which is directly reflected in service life in a dusty, cycling application. Running a marginally rated heater at the top of its range in this duty is the shortest path to a monthly replacement interval.
- Station envelope and mounting detail
- Nozzle count, orifice size and duct length
- Available supply voltage and phase
- Airflow in SCFH at the nozzle, plus guaranteed minimum flow
- Target outlet air temperature and acceptable tolerance
- Machine cycle rate and expected stop frequency
- Board grade, coating weight and single or double PE
Temperature Ranges and Process Objectives
| Process Stage | Temperature (ºF) | Temperature (ºC) | Basis | Note |
| Gable-top carton bottom flap PE activation (hot-air oven outlet) | 570-840º F | 300-450º C | typical | Gable-top machine builders publish hot-air bottom sealing but not a temperature. Industry-typical heater-outlet range. |
| Gable-top carton top flap PE activation (hot-air oven outlet) | 570-840º F | 300-450º C | typical | Separate top oven blowing a selective pattern on the gable flaps immediately before the high-compression sealing jaws. |
| Paper cup sidewall seam PE activation or preheat | 570-930º F | 300-500º C | typical | Builders differ here. Some seal the seam with hot air alone, others use hot air only to preheat the blank and close the seam ultrasonically, which shifts the setpoint lower within the range. |
| Paper cup and bowl bottom disc and skirt sealing | 570-930º F | 300-500º C | typical | The highest demand point on a cup machine. Several builders heat the bottom in two steps, and some run 350-500 C on heavier or double-PE board. Setpoint is normally PLC-selected by board weight. |
| Flat-blank container and lunch-box corner sealing | 570-840º F | 300-450º C | typical | Small heated area at the corner tabs, short cycle, heater mounted close to the folding tool. |
| Aseptic carton bottom sealing in the sterile zone | 570-840º F | 300-450º C | typical | Same PE activation duty, but the airstream is inside the sterile zone, so no combustion products are acceptable. Top is often sealed ultrasonically. |
| PE coating melt point at the board surface (reference only) | approx. 230-266º F | approx. 110-130º C | typical | Reference figure for low-density polyethylene. The board surface stays far below the air temperature because dwell is well under one second. |
Frequently Asked Questions
Machine builders in this sector typically run 300 to 450 C (570 to 840 F) at the heater outlet for gable-top flap sealing, and typically 300 to 500 C (570 to 930 F) for paper cup sidewall and bottom sealing. These are industry-typical operating ranges rather than published figures from the machine builders. The board surface itself never reaches those numbers because contact time is well under a second. Start from the range, then tune to your board weight, coating thickness, nozzle standoff and line speed.
Usually yes. Serpentine and Serpentine VI elements and JET and MAX assemblies are built to the same job description as the compact hot-air heaters commonly fitted to cup and carton machines: electrically heat a flowing air stream to several hundred degrees Celsius and hold it. Replacement is a mechanical and electrical fit question. Send us the station envelope, the mounting detail, the nozzle arrangement, the available voltage and the airflow, and we will confirm the fit.
Serpentine VI is rated to 1500 F (815 C) outlet air, in 5.0 kW, 6.0 kW and 8.0 kW power options, with a 240 V single-phase configuration listed, a maximum inlet pressure of 25 psi, a 304 stainless steel housing and a minimum flow of 60 SCFH for accurate control. It uses a triple-pass open-coil Serpentine element in a compact modular package.
It depends on airflow and target temperature, not on the board. Work it from the mass flow through the nozzle and the required temperature rise, then add margin for the duty cycle. For reference, SureHeat JET is offered in 3 kW and 8 kW, Serpentine VI in 5.0, 6.0 and 8.0 kW, and SureHeat MAX from 6 kW to 36 kW with up to six elements. A single cup-machine bottom nozzle usually sits at the low end; a multi-lane gable-top oven manifold is where MAX becomes the right answer.
Three causes dominate in this application. First, cycling: every stop-start or oven retraction is a thermal cycle on the element. Second, flow loss: a blocked filter, a kinked hose or a partly plugged nozzle starves the element while the controller keeps calling for heat, which drives the coil above its rating even though the measured outlet air looks normal. Third, contamination: board dust, paper fiber and PE vapor drawn into the inlet or deposited on the nozzle. Guarantee minimum flow, filter the inlet and keep the nozzle clean, and element life improves without changing anything else.
That is the normal duty for this equipment, and it is what the element construction has to be chosen for. Open-coil Serpentine elements have low thermal mass, which is why they ramp fast, and they are built to be cycled. Pair the heater with a controller that holds a standby setpoint during short stops rather than switching fully off, and the element sees a much gentler cycle while the station still comes back to the seal window in seconds.
Electric resistance heating adds no combustion products to the airstream. Whatever enters the heater is what leaves it, at a higher temperature. The cleanliness of the air is therefore set by your supply: filtered compressed air or a filtered blower feed. For sterile hot air on aseptic carton lines, SFI inline heaters and SureHeat MAX handle the higher temperature and pressure duty, and the airstream stays clean because nothing is burned in it.
Yes. SureHeat control panels are matched to the heater family. Serpentine VI is specified with digital temperature controllers using Type K thermocouples, and JET and MAX assemblies include dual Type K thermocouples with over-temperature protection. For a multi-station machine, each seal station should be controlled on its own loop so one nozzle does not set the temperature for all of them.
