Ammonia Cracking Heaters
Electric Process Heating for NH₃ Crackers and Hydrogen Production
Ammonia cracking is an endothermic reaction — it only runs if heat keeps going in. Delivering that heat electrically, at temperatures up to 1000°C, into a chemically aggressive nitrogen-rich gas stream, is where most standard heater designs fail.
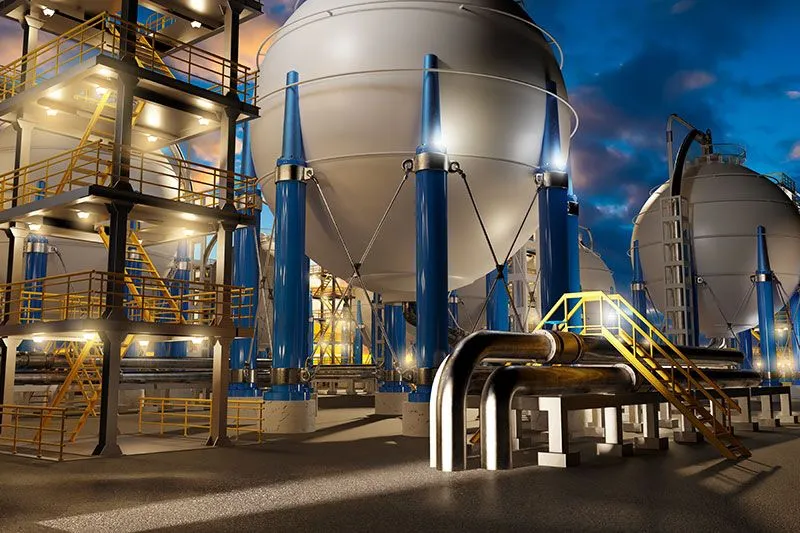
TUTCO SureHeat has spent over 50 years engineering electric air, gas and steam heaters for applications where off-the-shelf equipment does not survive. Our process heating solutions range from a few kilowatts to multi-megawatt systems, reach process temperatures above 1050°C (1922°F), and heat up in seconds rather than minutes. Every heater is engineered around the customer's specific pressure, temperature, flow and gas chemistry — which is exactly what ammonia cracking, NH₃ preheating and partial cracking for ammonia-fueled combustion demand.
Technical Specifications
| Parameter | Capability |
| Heating power | 5 kW to 3 MW+ (multi-megawatt via parallel units) |
| Maximum process gas temperature | up to 1050°C (1922°F) |
| Maximum design pressure | up to 200 bar (2900 psi) |
| Wetted materials | High-nickel alloys selected for nitriding resistance (Alloy 600 / 601 / 602 CA class), application-specific |
| Heat-up response | Process temperature reached in seconds |
| Control | Integrated SCR/thyristor control, multi-zone, closed-loop |
| Certification | ASME Section VIII, PED 2014/68/EU, CE, ATEX on request |
| Configuration | Specialty Flanged Inline (SFI), custom threaded inline, custom-engineered assemblies |
Why Ammonia Became the Hydrogen Carrier
Hydrogen is a strong clean energy carrier and a poor cargo. Its volumetric energy density is so low that moving it any real distance means compression or cryogenic liquefaction below −253°C — expensive, and technically demanding at scale. Ammonia (NH₃) solves the transport problem. It carries roughly 17.6% hydrogen by weight, offers around twice the energy density of compressed hydrogen gas, and liquefies at a comparatively mild −33°C at atmospheric pressure. Just as importantly, the logistics already exist: port terminals, tanker fleets, pipelines and storage built for the fertilizer industry form a ready-made backbone for hydrogen transport.
The remaining step is recovering the hydrogen at the destination. That step is ammonia cracking.
Ammonia Cracking: Turning NH₃ Back Into Hydrogen
Ammonia cracking — also called ammonia decomposition — is the thermal breakdown of NH₃ into hydrogen and nitrogen, typically producing a 75% H₂ / 25% N₂ stream. Industrial-scale NH₃ crackers are already operating as demonstrators, with further units planned at major import terminals, while green ammonia projects across the Middle East, Australia, China and Northern Europe build out the supply side.
Ammonia is also being used directly as a fuel. Shipping operators and engine manufacturers are developing ammonia-capable propulsion, and in most of these systems the ammonia is partially cracked before combustion — enriching the fuel stream with hydrogen to improve ignition reliability, flame stability and efficiency.
In every case the chemistry is carbon-free. Whether combusted directly, partially cracked, or fully decomposed for fuel cells or industrial hydrogen use, there is no CO₂ in the product — only nitrogen and water, provided NOₓ is properly managed.
Operating Temperatures for Ammonia Cracking
The temperature an ammonia cracking heater must deliver depends entirely on the process objective. The full working range looks like this:
| Process Objective | Typical Gas Temperature | Notes |
| NH₃ vaporization and preheating | 100 – 300°C | Liquid ammonia to vapour, feed conditioning |
| Catalyst inlet preheating | 300 – 450°C | Most common duty in catalytic crackers |
| Partial cracking for combustion | 400 – 600°C | Tunable H₂/NH₃ ratio for engines and burners |
| Catalytic full cracking | 600 – 800°C | Conversion efficiency rises with temperature |
| High-conversion / low-catalyst-activity systems | up to 1000°C | Approaching complete decomposition |
The higher end of this range is not a catalogue limitation — it is a materials question. Cracking will occur at these temperatures; whether the heater survives them in an ammonia atmosphere depends on alloy selection. That is the real engineering problem, and it is addressed below.
Nitriding: The Failure Mode That Defines the Design
The critical challenge in ammonia cracking heater design is not oxidation. It is nitriding.
As ammonia decomposes it releases highly reactive atomic nitrogen, which aggressively attacks iron-based alloys. This atomic nitrogen diffuses into metal surfaces and forms brittle nitride layers that lead to cracking, spalling and progressive structural degradation. Unlike oxidation — the dominant concern in most high-temperature applications — nitriding attacks from within the metal and is far harder to design around.
The practical consequence: standard stainless steels and common heating alloys that perform reliably elsewhere can lose most of their service life in an NH₃ cracker. Resistance to nitriding becomes the governing selection criterion, and it varies sharply with temperature, gas composition and alloy chemistry.
Material Selection Based on Real-World Testing
Nitriding resistance cannot be predicted reliably from standard corrosion data. Nickel and chromium content, along with stabilizing elements, shift performance in ways that published tables do not capture.
TUTCO SureHeat has therefore run dedicated test programmes, exposing candidate alloys to representative ammonia cracking atmospheres across the relevant temperature range and measuring degradation under conditions matching real process service. Those empirical results — not generic datasheets — are what drive our material selection.
Every wetted component is specified on this basis: heating elements, structural supports, internals and pressure vessel. Testing is ongoing, and the resulting knowledge base continues to expand heater performance and service life at the upper end of the temperature range.
Applications
Our ammonia cracking heaters are specified into:
Ammonia import terminals — NH₃ vaporization, feed preheating and cracker start-up heating
Industrial-scale NH₃ crackers — catalyst inlet preheating and supplementary process heat where waste-heat recovery is unavailable or during start-up and transients
Ammonia-fueled engines and burners — partial cracking to produce a controlled H₂/NH₃ mixture with stable composition across varying flow
Fuel cell hydrogen supply — full decomposition for on-site hydrogen generation
Pilot plants, demonstrators and R&D rigs — small-scale units with industrial-grade materials, allowing test data to scale
Electrified process retrofits — replacing fired heating where renewable electricity is available and CO₂-free operation is required
TUTCO SureHeat Ammonia Cracking Heaters
Our heaters for ammonia service are purpose-engineered, not modified standard products. Each system is designed around the specific application: temperature, pressure, flow rate, gas composition and control requirements.
Three things come together in every unit — material selection validated against nitriding, thermal design that controls element surface temperature rather than only outlet temperature, and mechanical engineering rated for pressurized service. This combination is what delivers the reliability and service life that ammonia cracking demands.
The result is a heater platform that scales from research rigs to full industrial hydrogen production, supported by installed units in ammonia and hydrogen applications across Europe, North America and Asia.
Project details remain confidential under customer agreements, but our engineering team can discuss comparable duties and configurations directly.
Get Started on Heating Solutions for Your Ammonia Cracking Application
Share information on your application and learn how TUTCO SureHeats’s precision heating solutions can optimize your operations.
Contact our engineering team today to design a custom thermal solution built for reliability, efficiency, and performance.
Frequently Asked Questions
Yes. Partial cracking requires precise, stable temperature control to hold a consistent hydrogen-to-ammonia ratio across changing flow conditions. This is a control and thermal design problem as much as a power problem, and it is a duty we engineer for specifically.
Full decomposition of NH₃ yields approximately 75% hydrogen and 25% nitrogen by volume, with residual ammonia and moisture depending on conversion efficiency. Hydrogen is typically purified downstream by pressure swing adsorption (PSA) where high purity is required.
Yes. Designs are available up to 200 bar, with pressure vessels engineered and certified for the application. Pressure rating, temperature and material selection are specified together, since all three interact in ammonia service.
A preheater raises the NH₃ stream to catalyst inlet temperature (typically 300–450°C) ahead of the reactor. A cracking heater supplies the heat that drives the decomposition reaction itself, at substantially higher temperatures. Both duties face the same nitriding environment, and both are within TUTCO SureHeat's scope - many projects use the same heater platform for each.
When ammonia decomposes it releases atomic nitrogen, which diffuses into metal surfaces and forms brittle nitride layers. These layers crack and spall, progressively destroying the component. Because heating elements run hotter than the process gas, they are the most exposed part of the system. Alloys that perform well against oxidation may fail rapidly against nitriding, which is why material selection must be validated by testing in representative ammonia atmospheres.
Electric process heaters produce no combustion emissions, start in seconds rather than minutes, offer far tighter temperature control, and can be driven by renewable electricity — keeping the hydrogen supply chain carbon-free end to end. They are also significantly more compact and can be remotely controlled, which matters in terminal and marine installations where space and manning are constrained.
It depends on the objective. Catalyst inlet preheating typically requires 300–450°C. Partial cracking for combustion applications runs at 400–600°C. Catalytic full cracking generally needs 600–800°C, and systems targeting near-complete conversion with reduced catalyst activity may require up to 1000°C. TUTCO SureHeat heaters cover the full range; the limiting factor at the top end is alloy selection, not heater capability.
